New Energy Wind Power Generation Model Manufacturing Process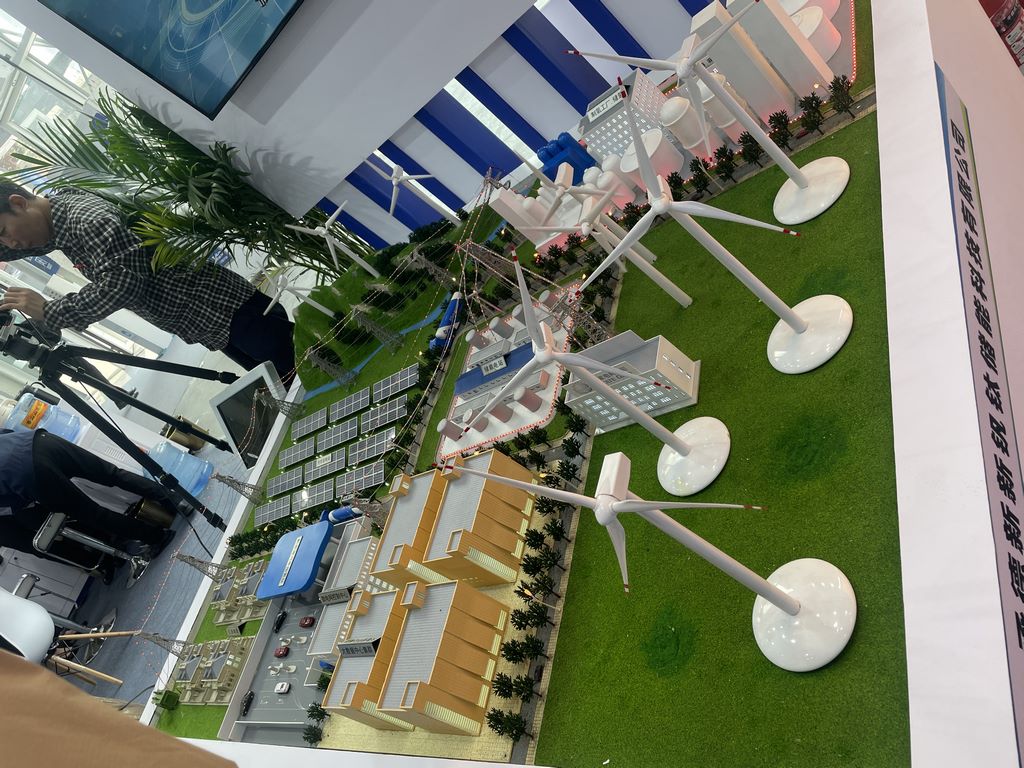
I. Material Preparation Stage
3mm-thick ABS engineering plastic sheets are selected as the base material, with 1mm-thick ABS sheets used for blades and other precision components. The tower cylinder is made from pre-fabricated ABS pipes (80mm diameter), with an internal 3D-printed ABS skeleton for structural reinforcement. All joints are seamlessly bonded using ABS-specific adhesive.
2. Core Component Processing
Tower Cylinder Manufacturing:
Cut the ABS pipes to a height of 1.2 metres
Use thermal bending to create the tapered transition section
Install reinforcement rings every 30 cm internally
Surface treated with 800-grit water sanding
Cabin Components:
CNC machining of the main structure
Manual finishing of the gearbox housing surface
Installation of miniature bearings to enable rotor linkage
Blade Forming:
Vacuum forming of the blade base
Manual grinding of the leading edge to a 0.2mm thin edge
Ultrasonic welding of internal reinforcement ribs
III. Surface Treatment Process
Pre-treatment:
Spray the entire machine with ABS-specific treatment agent
Electrostatic dust removal treatment
Coating Process:
Primer: Grey ABS-specific primer
Main colour: RAL7035 industrial grey
Logo layer: Screen-printed company logo
Protective layer: Matte polyurethane clear coat
Detail finishing:
Spot-painting of bolts with metallic paint
Warning stripes applied via laser-cut film
Aged finish applied to seams
4. Assembly and Testing
Dynamic System Assembly:
Install miniature DC motor
Configure gear reduction assembly
Magnetic coupling blade connection mechanism
Lighting System:
Navigation lights use SMD LED modules
Control box integrates light sensors
All wiring hidden within the tower cylinder
Final Testing:
Speed test (3-speed adjustable)
Lighting sequence programming
Vibration stability test


